Polyimide Label Substrate for Aerospace and Industrial Use
Table of Contents Polyimide Label Substrate for Aerospace and Industrial Use A polyimide label substrate is a high-temperature film construction that stays bonded and scannable
A polyimide label substrate is a high-temperature film construction that stays bonded and scannable through reflow, bake, and long service heat.
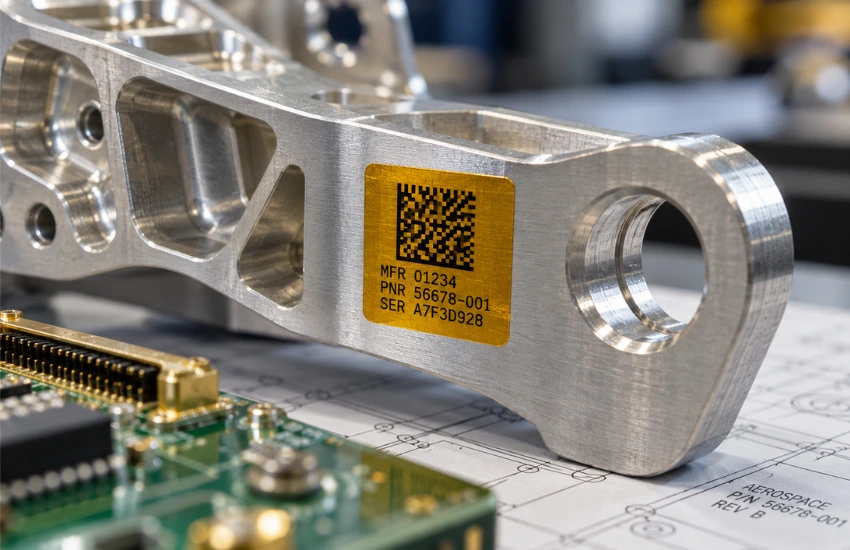
The common failure looks like this: a serialized bracket gets a clean Data Matrix label, goes through a paint bake, and comes out with a lifted edge, uneven yellowing, and a code that fails verification. That outcome is a traceability exception on a high-value part, a rework ticket, and a quality record to explain. It is almost never a printing problem. It is a materials problem: the label was specified for handling, not for the full process and service environment.
A polyimide label is a layered construction, not just a film, and its topcoat and adhesive usually set the real performance limit.
Polyimide is a high-performance engineering film known for dimensional stability and retained mechanical properties at elevated temperatures. In label form, the film is one layer of a four-part construction.
Polyimide base film
A thin, high-modulus polyimide film, often amber and translucent, though white and matte versions exist. The base film provides the dimensional stability at temperature that paper and polypropylene facestocks lack.
Printable topcoat
The receptive layer the converter applies so the surface accepts ink or thermal transfer ribbon. Ink and ribbon bond to the topcoat, not to the polyimide film itself, so topcoat choice controls printability and post-bake legibility.
Adhesive system
Commonly a silicone or high-temperature acrylic adhesive, selected for the specific thermal and chemical exposure. Silicone adhesives are often specified for reflow survivability; removable applications need a different adhesive entirely.
Optional overlaminate
A protective layer added over the printed image for abrasion, solvent, or fluid resistance where maintenance handling or chemical contact is expected.
The polyimide film is almost never the weak link. In real failures, the topcoat discolors or loses ink anchorage, or the adhesive softens, oozes, or loses tack after thermal cycling, long before the polyimide itself is stressed. Evaluating a high-temperature label film means evaluating the full stack, not a datasheet number for the base film.
Kapton film is DuPont’s brand of polyimide film. Specifying “Kapton label, aerospace” tells a supplier the material family, not the construction you need.
Each common label facestock fails under heat in a characteristic way; polyimide holds up longest through reflow, bake, and service heat.
Facestock family | Characteristic failure under heat | Typical thermal behavior (illustrative) | Chemical resistance | Relative cost tier |
Coated paper | Chars, embrittles, and discolors; adhesive and facestock degrade together | Low | Poor | $ |
Polypropylene (PP) | Shrinks and distorts well below most process bake temperatures | Low | Moderate | $ |
Polyester (PET) | Durable for general use; dimensional and topcoat limits appear at reflow and high-bake temperatures | Moderate to high | Good | $$ |
Polyimide | Holds dimensional stability and legibility through short high-temperature excursions and sustained service heat | Highest of the common pressure-sensitive label films | Very good | $$$– $$$$ |
Treat this table as qualitative and illustrative. Confirm performance against the supplier’s technical data sheet for the exact facestock, topcoat, and adhesive combination you intend to buy.
Label suppliers usually publish two different temperature ratings, and mixing them up is a common specification error.
Short-term excursion temperature
The rating that governs process steps such as solder reflow, paint bake, powder-coat cure, and wash cycles. Exposure lasts minutes.
Continuous service temperature
The rating that governs the asset’s working life, such as engine and nacelle-area heat soak, motor housings, and exhaust-adjacent brackets. Exposure lasts years.
A label can clear a reflow excursion and still fail a lower-temperature continuous soak, because adhesive creep and topcoat oxidation accumulate over time. Specify both temperature ratings, each with a dwell time, not one.
Aerospace programs call out polyimide labels where heat, aviation fluids, and decades of traceability combine on a single part.
Wire and harness marking
High temperature wire labels need a thin, flexible, solvent-resistant construction that survives bundling and installation handling without losing legibility.
Hydraulic and fuel system component identification
Labels exposed to hydraulic fluids, including Skydrol-type phosphate ester fluids, along with fuels and cleaning solvents.
Engine, nacelle, and bleed-air area components
Labels driven by sustained elevated service temperature rather than a single process spike, which makes the continuous service rating the governing number.
MRO, overhaul, and spares tags
Identification, often as heat resistant tags, for parts that move through repeated repair cycles and must stay identifiable years after the original build.
Serialized item marking
Unique identification that stays legible and machine-readable for the life of the asset.
Altitude and humidity cycling, de-icing chemical contact, and abrasion from maintenance handling add to these exposures. Together, they turn a specialty high temperature label material from a preference into a specification requirement.
Prime contractors and customers commonly reference item marking requirements such as MIL-STD-130 and wire-marking practices such as SAE AS5942 on drawings and purchase orders. These documents describe marking and identification practices; they do not make any particular film, ink, or press “qualified.” Verify applicability, revision, and acceptance criteria with your own QA organization and the controlling customer drawing.
Lead-free solder reflow is the driving constraint for board labels, which is why polyimide with a high-temperature adhesive is the standard.
Peak reflow temperatures for lead-free SAC alloys run higher than tin-lead profiles, and boards often see multiple reflow passes plus rework. Wave solder, aqueous cleaning, conformal coating cure, and burn-in add to that history, so a PCB label substrate has to clear a stacked thermal and chemical exposure, not a single event.
The real acceptance criterion for circuit board labels is not “did the label stay on.” It is the three measurements below.
2D code contrast and modulation after thermal exposure
Amber polyimide films and post-bake topcoat discoloration both reduce symbol contrast, so contrast must be measured after reflow, not before.
Quiet-zone integrity
Edge lift, adhesive ooze, and flux residue can encroach on the quiet zone around a 2D code and cause read failures even when the symbol itself is intact.
Verified scan grade
The grade measured on the actual reader and optics used downstream, not on a bench verifier alone.
ESD characteristics and outgassing behavior also matter for sensitive assemblies and sealed environments. Review both with your material supplier and your own process engineers rather than assuming them from the film type.
Polyimide is harder to print than PET, because ink adhesion depends on the topcoat, full cure, contrast control, and careful web handling.
Printability is a topcoat property
Untreated polyimide is a relatively low-surface-energy, chemically inert surface. Ink and ribbon adhesion depend on the receptive topcoat the converter applied, which is why two rolls both labeled “polyimide” can behave completely differently on press.
Thermal transfer on polyimide
Thermal transfer performance on polyimide is ribbon-dependent. Resin ribbons are typically required, and the ribbon-to-topcoat pairing drives smear and solvent resistance.
UV inkjet on polyimide
UV inkjet printing on polyimide film depends on wetting, drop control, and complete cure. Under-cured UV ink can pass a handling check and then fail after a bake, so cure must be verified on the post-process sample.
Amber base color and code contrast
The native amber of many polyimide films reduces contrast for dark-on-light codes. The fixes are a white-topcoated polyimide, an opaque white underprint beneath the code from a press with a white ink channel, larger module sizes, or a symbology change. UV label printers with white ink can lay down that opaque underprint in the same pass as the code. Settle the approach during qualification, not after a rejection.
Thin, high-modulus web handling
Thin-gauge polyimide is stiff but unforgiving: tension control, static control, and clean die cutting and matrix stripping all need attention. High-modulus films resist matrix break and can spring back, which shows up as waste. Short ramp-up runs and documented press profiles per substrate protect an expensive material budget.
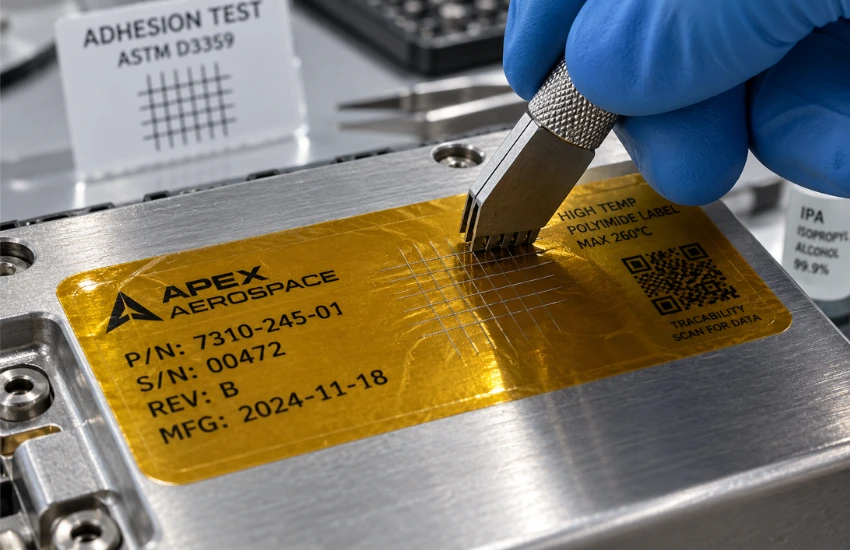
Verify ink adhesion on polyimide rather than assuming it. These four checks catch the most common print-side failures.
Check | How to run it | What it catches |
Cross-hatch tape test | On freshly printed and on fully cured samples | Weak ink anchorage to the topcoat |
Solvent rub | With the cleaning agents actually used in your build and MRO processes | Ink or topcoat that softens under process chemistry |
Post-bake or post-reflow re-check | Legibility and barcode grade measured after the real thermal step | Contrast loss, discoloration, and quiet-zone encroachment |
Abrasion check | Wherever maintenance handling is expected in service | Image wear that would break traceability over the asset’s life |
Define the worst-case thermal and chemical profile, trial the exact construction on your real process, then release it to the program.
Step 1: Define the worst-case thermal profile
Combine every process excursion (reflow, bake, wash) with the continuous service temperature and its dwell time.
Step 2: List every chemical, fluid, and cleaning exposure
Include solvents used at MRO and overhaul, not just the chemistry the label sees at initial build.
Step 3: Define code and legibility acceptance criteria
Set symbology, module size, minimum scan grade, and human-readable legibility requirements for your high temperature barcode labels before any material is printed.
Step 4: Print a trial on the exact construction
Use the exact substrate, adhesive, and topcoat combination you intend to buy, not an equivalent.
Step 5: Run samples through the real process step
Use your oven, your reflow profile, and your wash chemistry rather than a generic lab condition.
Step 6: Re-verify, document, and release
Re-check adhesion, legibility, and scan grade, document the result, and release the qualified material to the program.
Operations automation earns its keep at step 6 and beyond: tying revision-controlled label templates, serialization, and on-demand print release to production scheduling, so the right label (correct revision, correct serial, correct substrate) is produced at the point of need instead of pulled from a shelf of pre-printed stock. Bringing that work onto in-house digital label printers also removes converter minimum order quantities and multi-week lead times from short-run programs.
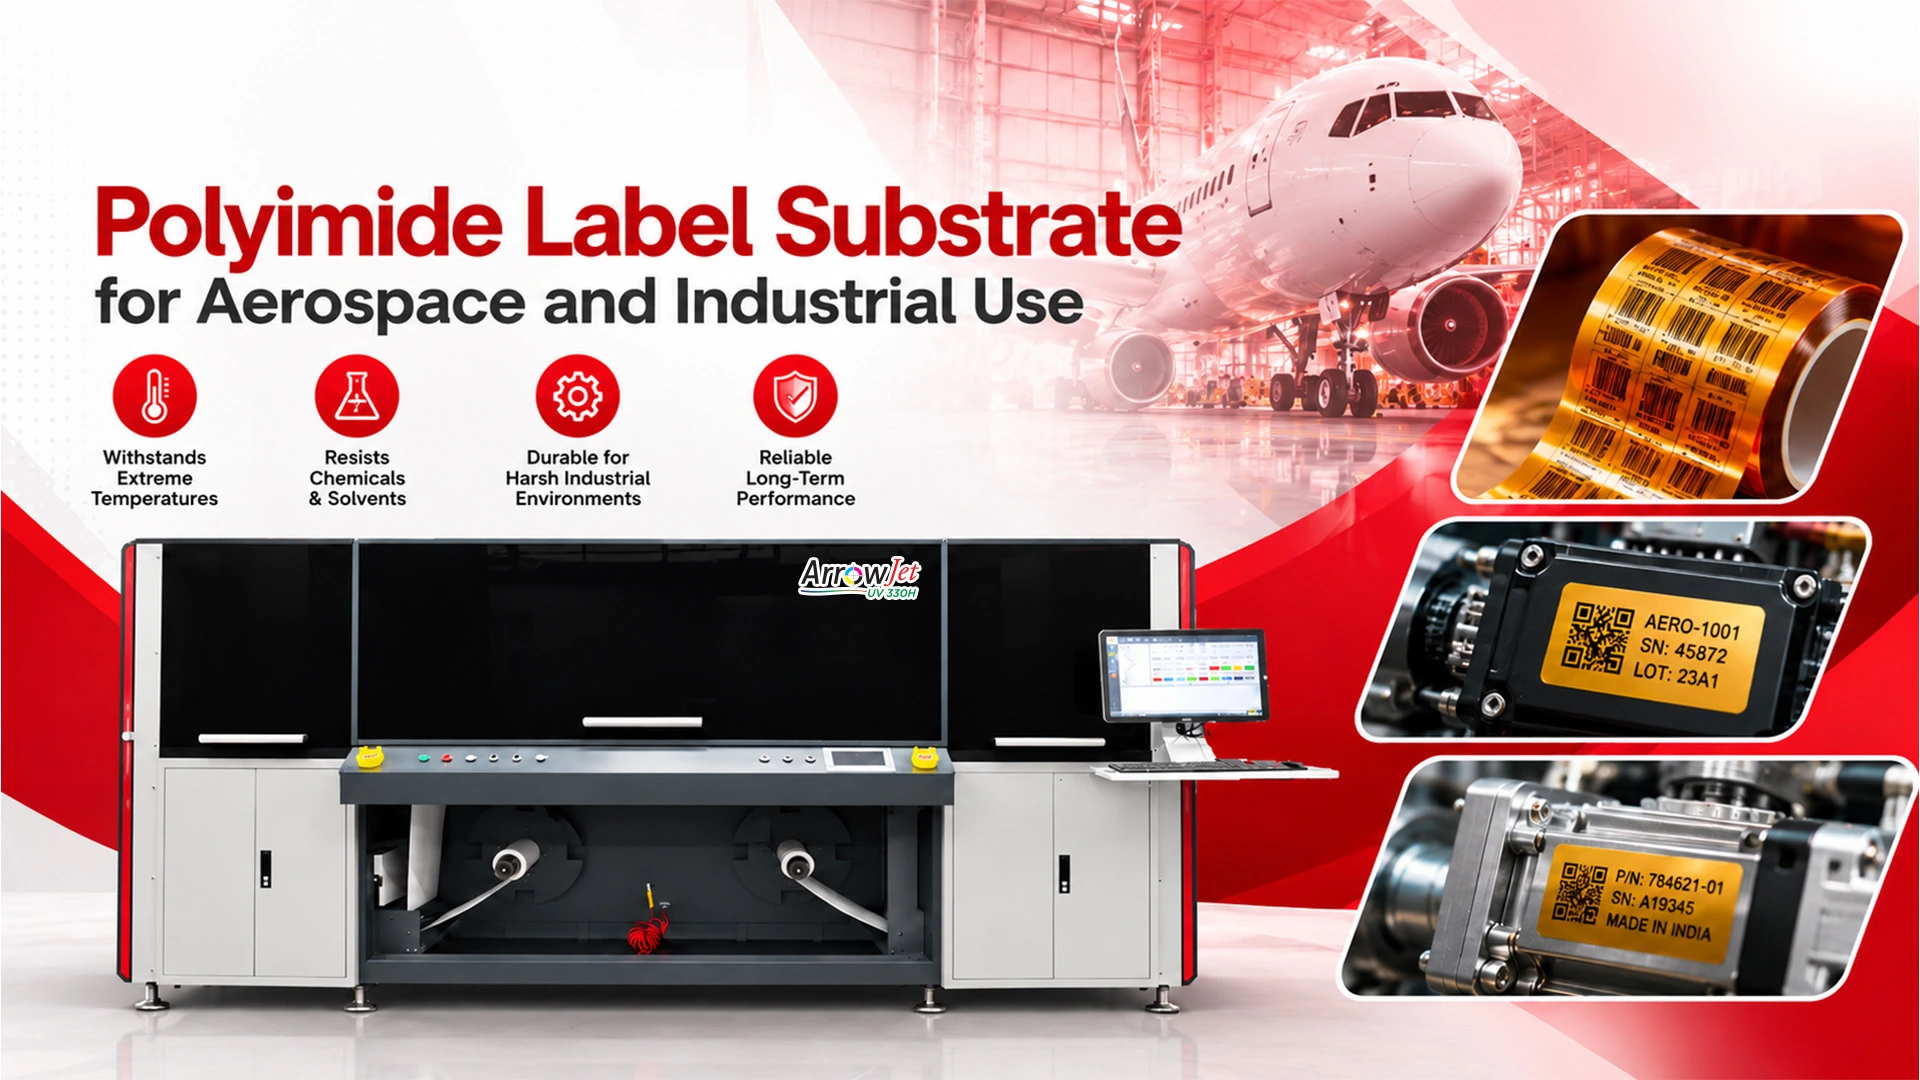
The ArrowJet UV 330H is a hybrid UV LED label press for short-to-medium runs, suited to serialized, high-mix specialty film labels.
The ArrowJet UV 330H, from Arrow Systems, an industrial label printing and marking systems integrator, is a true hybrid UV label press that combines roll-to-roll production with flatbed printing in one system. It is built for short-to-medium runs, which matches the profile of most aerospace, defense, and EMS label programs: many part numbers, variable serials, and frequent substrate changes across specialty films, including high-heat label constructions.
UV LED curing for fast test turnaround
UV LED curing polymerizes the ink immediately after printing, so a trial sample can move to finishing or a test oven without a drying wait. Complete cure remains a qualification check on polyimide, as covered above.
CMYK + White for amber polyimide contrast
The ArrowJet UV 330H runs CMYK + White, CMYK + Varnish, or CMYK + White + Varnish configurations. Opaque white supports printing on clear, metallic, and dark substrates, and provides the underprint option for raising code contrast on amber or translucent films.
Corona treater and web cleaner
The press includes a corona treater and a web cleaner. Corona treatment can help ink wetting on film surfaces, but on polyimide the converter’s topcoat remains the baseline for adhesion, so results are confirmed in a substrate trial.
Zoned inspection vacuum bed
A zoned inspection vacuum bed holds media flat and keeps CMYK, white, and varnish layers in registration, preventing curling and lifting of thin films and specialty media.
Variable data printing for serialization
The ArrowJet UV 330H supports variable data printing for barcodes and QR codes, enabling sequential serials and per-part labels within a single run. Paired with revision-controlled label data and print release triggered from production scheduling, the press supports an on-demand model for MRO tags, prototype builds, and per-serial marking.
Flatbed mode for tags, plates, and samples
Flatbed mode prints on a 350 mm × 1500 mm area and accepts rigid media up to 50 mm thick, which covers sheet-fed tags and prototype samples alongside roll labels.
Specification | ArrowJet UV 330H |
Printing modes | Roll-to-roll and flatbed |
Printhead type | Ricoh Gen6, piezo inkjet drop-on-demand |
Ink configurations | CMYK + White, CMYK + Varnish, or CMYK + White + Varnish |
Curing | UV LED |
Maximum print resolution | Up to 720 × 4800 dpi |
Minimum droplet size | 5 pl, with grayscale support |
Maximum print width | Up to 330 mm |
Maximum media width | 350 mm |
Maximum roll diameter | 450 mm on a 3″ core |
Flatbed printing area | 350 mm × 1500 mm |
Maximum media thickness (flatbed) | 50 mm |
Printing speed | 20 ft/min |
Variable data printing | Barcode and QR code supported |
Web treatment | Corona treater and web cleaner |
RIP software | Onyx |
Power supply | 220V single phase, 50/60 Hz |
Because polyimide printability depends on the topcoat, confirm fit empirically before choosing any polyimide label printer. Run your actual film, adhesive, and code requirements through a substrate trial, then evaluate ink adhesion, cure, contrast, and post-process scan grade against your acceptance criteria before making an equipment decision.
Common questions from aerospace, defense, and electronics teams specifying polyimide labels for high-temperature traceability.
Kapton is DuPont’s brand name for a family of polyimide films, so the two terms are often used interchangeably, but they are not equivalent for specification purposes. Polyimide label stock is available from multiple film producers and converters in different gauges, colors, topcoats, and adhesive systems, and two polyimide label products can perform very differently in ink adhesion, removability, and chemical resistance. Specify the full construction (film type and gauge, topcoat, adhesive, and any overlaminate) and confirm performance against the supplier’s technical data sheet.
Polyimide label constructions are widely used for board-level identification through lead-free reflow, but survivability depends on the full construction, not the film alone. The adhesive system, topcoat, and printed image typically limit performance before the base film does, and reflow profile, number of passes, board mass, and downstream cleaning or conformal coating all affect the result. Test the printed label on your actual board through your actual profile, then re-verify adhesion, edge lift, and 2D code scan grade.
PET or high-temperature paper is often sufficient, and less expensive, when the label sees only moderate process temperatures, brief heat exposure, and limited chemical contact, and does not need to stay readable for the asset’s full service life. Move to polyimide when the label must clear solder reflow or a high-temperature bake, endure sustained elevated service temperature, resist aggressive fluids and solvents, or hold machine-readable traceability for years. Define the worst-case combined thermal and chemical profile first, then let that profile select the substrate.
Post-bake verification failures usually trace to the topcoat or adhesive rather than the polyimide film. Topcoat discoloration and the native amber of many polyimide films reduce symbol contrast, while edge lift, adhesive ooze, or flux residue can encroach on the quiet zone. Set acceptance criteria as scan grade measured after the real process step, and address contrast during qualification with a white-topcoated film, an opaque white underprint, larger module sizes, or a symbology change.
Specification confidence comes from testing, not datasheets. Send Arrow Systems your actual polyimide substrate, thermal profile, chemical exposures, and code requirements, and receive printed samples from the ArrowJet UV 330H to evaluate ink adhesion, cure, contrast, and post-process legibility on your own material before any equipment decision.
Arrow Systems also offers a structured, no-obligation press assessment covering your substrate list, typical run lengths, symbology and serialization requirements, and finishing needs, so you can size an in-house label production setup for short-run aerospace, defense, and PCB labels.
Table of Contents Polyimide Label Substrate for Aerospace and Industrial Use A polyimide label substrate is a high-temperature film construction that stays bonded and scannable
Table of Contents Entry-Level Label Printer for a Supplement Brand: Readiness Guide A supplement brand is ready for an entry-level label printer when it passes
Table of Contents Cannabis Label Versioning Workflow for Multi-State Brands A cannabis label versioning workflow produces state-specific labels from one master template by moving state-variable
Table of Contents Water-Based vs UV-Cured Label Adhesive: Food & Pharma Guide Water-based adhesives suit dry, ambient containers; UV-cured hot melts suit cold, wet, curved
Table of Contents Is Your Confectionery Brand Ready to Bring Flexible Packaging In-House? In-house flexible packaging pays off for confectionery brands with many SKUs, short
Table of Contents Label Slitting and Matrix Removal: Where Converters Lose Finishing Time Label slitting and matrix removal, plus rewinding, cost converters more finishing time