Curled beer label on a chilled bottle showing cold-storage adhesion failure.

Table of Contents

Beer Label Curling in Cold Storage: Diagnose the Mismatch

Beer label curling in cold storage signals a facestock, adhesive, or application mismatch — rarely just one bad label roll.
Key Takeaways

  • Curl and edge lift are two different failure modes with two different root causes — the peel test, which shows where the adhesive stayed, tells you which one you’re looking at.
  • Cold, dry air pulls moisture out of paper facestock while adhesive tack and flow drop at the same time — coolers create both stresses at once, which is why ambient units from the same run rarely fail.
  • Film facestocks (BOPP, PP, PE) remove the dimensional-movement driver entirely; cold-temperature adhesives address the tack-and-flow side — matching both to your SKU’s aesthetic and cold-chain exposure is what actually holds up.
  • Logging spec-sheet detail (facestock type, adhesive class, minimum application temperature, service range) and application conditions (room humidity, container surface temperature, time to chill) on every run turns a repeat failure into a traceable variable instead of a guessing exercise.
  • ArrowJet Aqua 330R prints short qualification runs across multiple candidate substrates with your own artwork, so a brewery can validate a material spec in its own cooler before standardizing a SKU on it.

Why Beer Labels Curl: Substrate Movement and Adhesion Failure at Low Temperature

Paper facestock shrinks as cold, dry air pulls out moisture while the adhesive layer holds still, and container curvature adds mechanical load.

Facestocks move dimensionally; adhesive layers do not. Uncoated and coated paper facestocks absorb and release moisture with the surrounding air. Move a labeled bottle from a humid packaging room into a dry cooler, and the paper gives up moisture and shrinks slightly. The adhesive film underneath does not shrink with it, so tension builds and concentrates where resistance is lowest — edges and corners.

Adhesives get stiff before they get weak. Pressure-sensitive adhesives depend on flow to wet out a surface. As temperature drops toward the adhesive’s minimum application temperature and lower service limit, tack and flow fall off. A cold-temperature pressure-sensitive adhesive is formulated to keep flowing in that range. A general-purpose permanent may simply lose the ability to relax the shrink tension the facestock is creating.

Container geometry adds mechanical load. Small-diameter bottles, high-crown cans, and shoulder placements force a flat label onto a curve. That spring-back concentrates stress at the corners. It is why curl and flagging often show up on 12 oz bottles first while the same material holds on a straight-wall can.

Three Failure Modes and What Each One Points To

Left undiagnosed, a cold storage label failure keeps repeating every time the SKU reaches the cooler, because the underlying variable never gets isolated. The three patterns below point to three different suspects.

Failure Mode

Where It Starts

Peel Test Result

Likely Cause

Curl

Symmetrical across leading and trailing edges, or all four corners

Adhesive stays on the container

Facestock dimensional movement

Edge lift / peel

Starts at one edge only

Adhesive comes away with the facestock

Incomplete wet-out, or an adhesive used outside its service or application window

Flagging

Label ends stand off a curved surface without fully separating

Label does not fully separate

Container diameter, web tension, or application pressure and dwell

Diagnosing the Mismatch: A Step-by-Step Sequence

Run this seven-step sequence on real failed units before changing any material — it separates substrate, adhesive, and process causes.

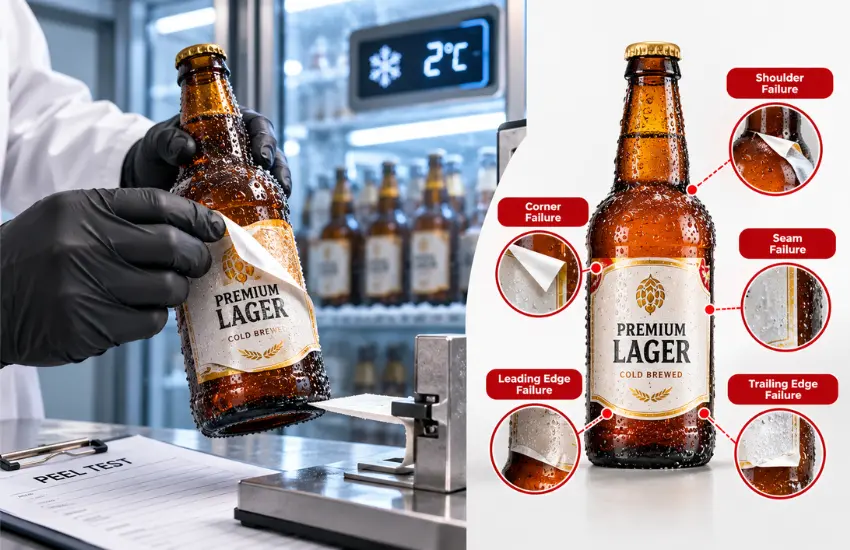
Peel test diagnostic sequence for beer label curl and adhesion failure.

Step 1: Pull 10 to 20 failed units

Record where the failure starts on each one — corner, leading edge, trailing edge, seam, or shoulder — and photograph it.

Step 2: Run the peel test

Lift a failed label and note where the adhesive stayed. Adhesive on the glass or aluminum indicates facestock-driven curl. Adhesive on the label back indicates low-temperature adhesion failure or poor wet-out.

Step 3: Compare cooler and ambient units from the same run

If the ambient units are clean and the cooler units are not, the trigger is temperature or humidity change, not the labeler.

Step 4: Compare formats

Check bottle against can, and across diameters and label sizes. Failures that track one container geometry are mechanical, not chemical.

Step 5: Segment by SKU, run, roll, and shift

A single roll or single shift failing points to a material lot or operator setup, not the specification.

Step 6: Read the spec sheet

Confirm facestock type, adhesive class, minimum application temperature, service-temperature range, caliper, and liner. If the sheet says only “paper, permanent,” you do not yet have a specification.

Step 7: Log the environment

Capture packaging room temperature and relative humidity, container surface temperature at the labeler, and elapsed time from labeling to entering the cooler.

Log steps 6 and 7 on every run. Without that record, the next failure turns into another guessing exercise.

Humidity Before Cold: The Application Environment Most Teams Skip

A correctly specified label substrate can still fail in the cooler if it was applied to the wrong container surface or humidity condition.

Wet or cold glass and aluminum

Containers coming off a rinser, filler, or pasteurizer often carry a film of water or condensation. That boundary layer keeps the adhesive from contacting the container, so you get a partial bond that looks fine and releases later. Cold containers also chill the adhesive on contact, cutting flow at the exact moment wet-out has to happen.

High-humidity packaging rooms

Summer packaging days can drive paper facestocks to a high moisture content before the pallet ever reaches the cooler. The larger the humidity delta between application and storage, the more shrink tension you build. Conditioning rolls in the room where they will run helps, but it does not erase the delta.

Pressure and dwell

Under-set nip pressure, worn brushes, or short roller contact leaves air pockets and low-contact areas. Verify pressure and dwell at changeover, not just label placement.

Time to chill

Many pressure-sensitive adhesives keep building bond strength for hours at ambient temperature. Moving pallets into a cold room soon after labeling can lock in a partial bond. Where the schedule allows, holding labeled product at ambient before chilling is one of the cheapest controls available.

Material Combinations That Hold Up in Refrigeration

Label facestock choice removes or adds the dimensional-movement driver; adhesive class decides whether the bond can relax cold-induced tension.

Facestock Options, Paper Against Film

Uncoated and felt or textured papers

Strongest craft aesthetic. Highest moisture absorption and dimensional movement. Most prone to curl and edge damage through condensation cycles.

Coated papers

Better surface durability than uncoated. Still moisture-permeable through edges and back. Often improved by a laminate or varnish.

BOPP label film, PP, and PE films

Dimensionally stable and moisture resistant, which removes the primary curl driver. Clear and white film look different from paper and may require design changes.

Adhesive Classes, By Function Rather Than Brand

Pressure sensitive label adhesive is the trade term; a search for cold weather adhesive or pressure sensitive adhesive label is usually describing the same problem. The classes below are grouped by function, not brand.

General-purpose permanent

Adequate for ambient dry-shelf SKUs.

Cold-temperature or low application temperature

A cold temperature adhesive, the class built for low temperature applications, is formulated to wet out on chilled containers and hold through refrigeration.

Wet-strength or ice-bucket oriented

Intended for immersion and repeated condensation cycles.

What to Request From Your Label Supplier

  • Facestock type, caliper, and coating or topcoat
  • Adhesive class and chemistry family, emulsion or hot melt
  • Minimum application temperature
  • Service-temperature range, including immersion exposure
  • Recommended container surface condition: dry, damp, or chilled
  • Laminate or varnish options for condensation and cooler abrasion
  • Liner type and roll conditioning guidance

An Illustrative In-House Validation Protocol

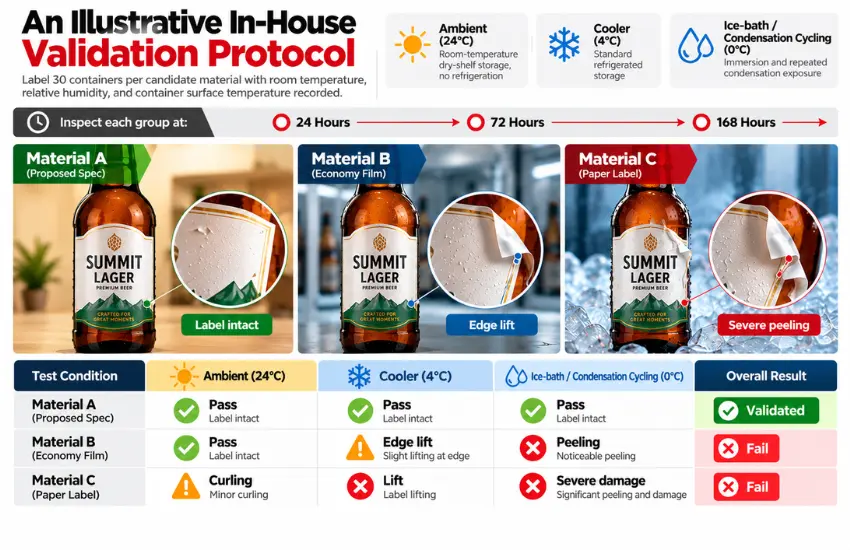
Offered as an example rather than a published standard: label 30 containers per candidate material with room temperature, relative humidity, and container surface temperature recorded.

Validation Group

Conditions Tested

Ambient

Room-temperature dry-shelf storage, no refrigeration

Cooler

Standard refrigerated storage

Ice-bath / condensation cycling

Immersion and repeated condensation exposure

Inspect each group at 24, 72, and 168 hours, and mark curl or lift by location on a simple diagram. The material that holds across all three groups becomes your validated spec for that SKU family.

In-house cold-chain label validation results across ambient, cooler, and ice-bath conditions.

Where the ArrowJet Aqua 330R Fits in Cold-Chain Label Specification

Short qualification runs on real substrates make cold-chain material testing economical, tying each validated stock to its SKU through production.

The hard part of a cold-chain material change is qualification economics. Traditional pre-printed buys make it expensive to test paper against film against a topcoated stock, so breweries keep running whatever is already on the shelf. The ArrowJet Aqua 330R, a water-based inkjet label press from Arrow Systems, changes that math in a few practical ways.

The equipment behind your digital label printers determines whether a validated material spec actually holds once a run leaves the qualification stage and reaches production volume.

Short qualification runs across candidate substrates

In-house beer label printing across several candidate substrates, using your own artwork, means you evaluate real labels in your cooler instead of blank swatches.

SKU-to-material discipline

Seasonal and limited-release runs stay on the validated stock rather than a leftover roll from an unrelated job.

Traceability through operations automation

Variable data and batch linkage tie substrate, adhesive spec, material lot, and shift to each run, so a future failure narrows to a lot instead of a season.

Built for food and beverage label production

The Aqua 330R is Nestlé Guidance Compliant and runs Food & Beverage, Cosmetics, Pharmaceutical, Nutraceutical/Supplement, and Flexible Packaging applications, so a beer-label qualification run sits on a platform already established in food-contact packaging.

Speed and format range from qualification to production

Three speed tiers (90, 150, and 195 ft/min) and a maximum media width of 380mm cover most beverage label formats, so the same press that prints a short qualification run can also run the validated SKU at production volume once the material spec is confirmed.

Substrate and adhesive suitability still has to be confirmed in your own cold-chain conditions. Printing capability shortens the loop; it does not replace the test.

Frequently Asked Questions — Beer Label Curling in Cold Storage

Common questions from brewery packaging, production, and quality teams diagnosing label curl and adhesion failures in cold storage.

The cooler changes two things at once. Cold air is typically drier, so a paper facestock releases moisture and shrinks slightly while the adhesive layer stays put, creating edge tension. At the same time, the temperature drop reduces adhesive tack and flow, so the bond can no longer relax that tension. Ambient units never see either stress, which makes side-by-side ambient and cooler samples from the same run the single most useful comparison available to you.

Start with the peel test and the segmentation check. If adhesive stays on the glass and curl is symmetrical, you are looking at facestock movement, which is a material specification issue. If adhesive comes away with the label and lift starts at one edge, suspect wet or chilled container surfaces, low nip pressure, or short dwell. Then check whether failures cluster by roll, shift, or container diameter. Material problems appear across the run; process problems usually track one setup, operator, or format.

Film facestocks remove the biggest curl driver, because BOPP, PP, and PE barely move with humidity. That is a real advantage in coolers and ice baths. But film alone does not fix an adhesive applied to wet glass, insufficient application pressure, or immediate chilling after labeling, and it changes the tactile and visual character many craft brands are built on. Teams often get further by matching a cold-temperature adhesive and the right topcoat to the look they want, then validating that combination in their own conditions.

Get a Cold-Chain Labeling Review from Arrow Systems

Bring the evidence: failed units, current label spec sheets, packaging-room temperature and humidity logs, and the list of affected SKUs. That is enough to run a structured cold-chain label review with Arrow Systems and trace a beer label curling cold storage failure to substrate, adhesive, or application environment.

The review defines a material specification you can test, and shows how short qualification runs on your own artwork can validate a substrate before you commit a SKU to it.