Is Your Confectionery Brand Ready to Bring Flexible Packaging In-House?
Table of Contents Is Your Confectionery Brand Ready to Bring Flexible Packaging In-House? In-house flexible packaging pays off for confectionery brands with many SKUs, short
In-house flexible packaging pays off for confectionery brands with many SKUs, short reorders, and frequent artwork changes, not high footage alone.
The question usually surfaces after a converter’s minimum order or a label-press assumption, and neither moment is a decision on its own.
Digital printing on flexible packaging changes the economics for some confectionery portfolios and not for others. This guide is written for confectionery brand owners, co-manufacturers, and the ops, engineering, QA, and packaging leads who have to live with the decision, plus the executive who signs the capital request. It gives you three go/no-go triggers, a landed-cost worksheet you can fill in with your own invoices, and a nine-point readiness checklist before you evaluate any digital flexible packaging printer.
Moment one: the converter minimum order
A converter quotes a minimum order quantity (MOQ) that locks you into nine months of printed film for a Valentine’s gummy with a six-week selling window.
Moment two: the label-press assumption
Your team, already running a roll-label press in the plant, assumes stand-up pouches are the same job on a wider web.
Neither moment is a decision. Both are symptoms.
Label press experience does not carry over to wide-web flexible packaging, because substrates, finishing chains, and failure modes all change.
Running a digital label printer does not qualify you to run a wide-web flexible packaging printer. The substrates behave differently, the finishing chain is longer, and the failure modes shift from cosmetic to functional. A bad label is ugly. A bad seal is a product loss.
Factor | Roll label in-house | Flexible pouch in-house |
Web width | Narrow web, sized to label die layouts | Wide web sized to pouch layouts, gussets, and multiple lanes |
Substrate | Pressure-sensitive face stock on a liner, dimensionally stable | Unsupported films, laminates, and metallized barrier structures with stretch and static behavior |
Ink and adhesion | Adhesion to coated PS stock; topcoat compatibility is well understood | Adhesion plus crease and flex resistance on treated films; surface energy and dyne level matter |
Tension and registration | The liner carries the web, so tension is forgiving | Thin, stretchy film; tension control drives registration and repeat length |
Downstream steps | Laminate, die-cut, slit, rewind — often inline | Lamination to a sealant web, slitting, then pouch making or supply as rollstock to a filler |
QC scope | Print defects, barcode grade, color match | All of that plus seal integrity, lamination bond, barrier performance, and print survival through forming and filling |
Operator skill | Label press operation and finishing | Web handling on film, tension and lamination judgment, plus converting coordination |
Two implications matter for candy brands.
Printing in-house does not mean pouch making in-house
Many brands produce printed rollstock internally and either keep converting with a pouch maker or feed film straight to a vertical form-fill-seal or flow-wrap line.
The QC plan has to grow
Seal and barrier verification is not a print function, and it needs a named owner.
In-house digital flexible packaging printing pays off with many SKUs, short reorders, and frequent artwork revisions, not annual footage alone.
Total annual volume is the number finance reaches for first, and it is the least useful input. Four inputs actually drive the answer:
Run length per SKU per order
The quantity you would buy on one purchase order, not annual usage.
Active SKU count and churn
How many SKUs exist, and how many are new, seasonal, or retailer-specific each year.
Reorder frequency
Four small pulls a year per SKU behaves nothing like one large pull.
Annual linear footage by structure
Group footage by film structure, because each structure carries its own qualification work and its own minimum order.
Portfolio type | Typical profile | Likely answer |
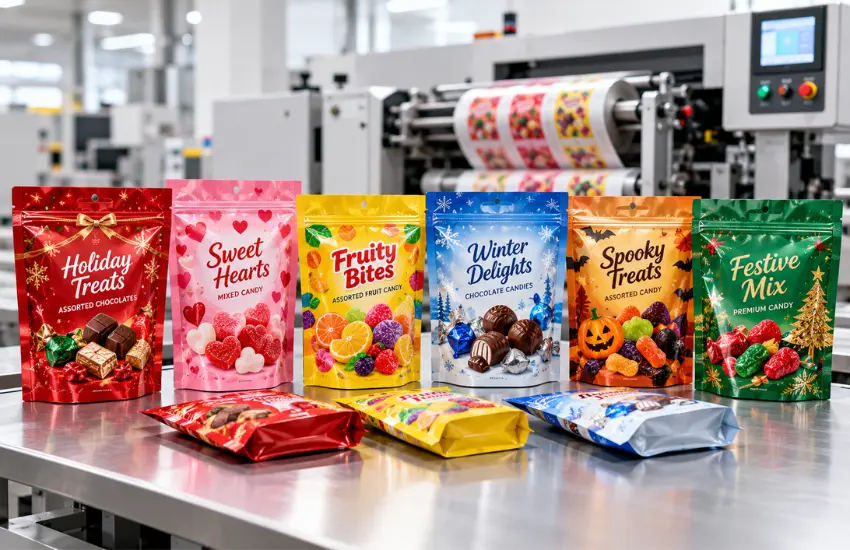
Favors in-house | Dozens of active SKUs, short runs in the hundreds to low thousands of pouches per order, seasonal waves around Halloween, winter holidays, Valentine’s Day, and Easter, frequent flavor tests, and regular net-weight, allergen, or promotional-flash revisions | Build the in-house business case |
Stays outsourced | A handful of core SKUs running long, stable orders on one or two qualified structures, with artwork that changes once every few years | Keep the converter relationship |
If a few SKUs carry most of your footage and rarely change, a converter will beat you on unit cost and you will not recover the capital. Say that out loud before you build the business case.
Teams often find that figure larger than the price-per-foot concession they spent the whole quote cycle negotiating. For the sachet-format view of the same problem, see Arrow’s guide to the real cost of SKU proliferation in sachet packaging.
Format variety, not volume, is what an in-house press solves when a portfolio spans several film structures and dozens of graphics.
Confectionery portfolios diverge hardest from the brands that flexible packaging economics were originally built around. Open your SKU sheet and count how many of these confectionery flexible packaging formats you actually run:
Stand-up pouches and gusseted pouches
Printed stand-up pouches and side-gusset formats for gummies, sour belts, and mixed bags, from share size through resealable family bags.
Flow-wrap film
Flow wrap packaging for bars, single-twist hard candy, and individually wrapped pieces.
Club multipacks and warehouse-channel variants
Different counts, net weights, and retailer marks on one recipe.
Private-label versions
A single base formulation, each version needing custom printed flexible packaging with its own artwork, brand-owner approval cycle, and revision schedule.
Seasonal graphics and limited editions
Tied to a retail window that closes whether your film arrived or not.
Flavor-test runs
A few hundred units for sampling, e-commerce, or one account.
Gummies
Gummies push toward moisture and oxygen barrier and need a sealant that survives sugar dust and oil in the seal area.
Chocolate
Chocolate is heat- and light-sensitive and sits in a different structure conversation entirely.
Hard candy
Hard candy is unforgiving about moisture ingress.
Every structure change restarts qualification, which is exactly why a converter-managed portfolio with many structures feels slow. If your formats and structures are few and stable, format variety is not your trigger. If you are managing several structures across dozens of graphics and multiple pouch styles, format churn, not volume, is what an in-house press solves.
Compare total landed cost, not price per thousand, because the lines a converter quote leaves out are usually where the money sits.
Build this worksheet from your own finance and procurement data, covering one year, with actuals wherever possible:
Cost line | Outsourced (annual) | In-house (annual) |
Printed film / rollstock purchase price | — | |
Plates or cylinders per SKU per revision | — | |
Minimum-order overage never consumed | — | |
Obsolescence from artwork, net weight, allergen, or retailer changes | — | |
Inbound freight | (film only) | |
Warehousing and handling of film inventory | (reduced) | |
Expedite and rush premiums | — | |
Revenue impact of missed seasonal or promotional windows | — | |
Equipment, installation, and training | — | |
Substrate, ink, and lamination consumables | — | |
Prepress and color management labor | — | |
Floor space, utilities, and material handling | — | |
Maintenance and service coverage | — | |
Scrap during substrate qualification and startup | — | |
Converting or pouch-making fees (may remain in both columns) | ||
Total landed cost |
Obsolescence and minimum-order overage
Together they often outweigh the price-per-foot gap under negotiation.
Expedite premiums and missed windows
These are the hardest lines to source and frequently the largest.
Qualification scrap on the in-house side
Qualification scrap is real, so budget film and press time for it instead of discovering it in month two.
If the totals land within a few percent of each other, the honest answer is not yet. Bring printing in-house when the gap is decisive and when the non-cost benefit, days rather than weeks from approved artwork to sellable pouch, justifies the operational load. For a broader view of the economics, see Arrow’s article on the real cost savings of in-house short-run digital printing.
In-house pouch printing fails on process discipline more often than on equipment, so any unchecked item below is a fix-first item.
Work through these nine prerequisites honestly. Anything unchecked is a fix-first item, not a launch item.
One caveat no equipment decision removes: substrate suitability, migration, food-contact status, and labeling content must be validated with your film supplier, your co-manufacturer, and qualified regulatory counsel against FDA food-contact and US labeling requirements. Equipment capability and regulatory compliance are separate questions, and they need separate owners. Arrow Systems sells printing hardware and does not provide regulatory or compliance advisory services.
The ArrowJet Aqua 800M is Arrow Systems’ wide-web water-based inkjet printer for digital flexible packaging printed in-house.
Arrow Systems is an industrial label and flexible packaging printing equipment supplier. The Aqua 800M is a water-based inkjet printer built for brands and co-manufacturers that want flexible packaging printing on the plant floor rather than in a converter’s queue.
The workflow it is built around
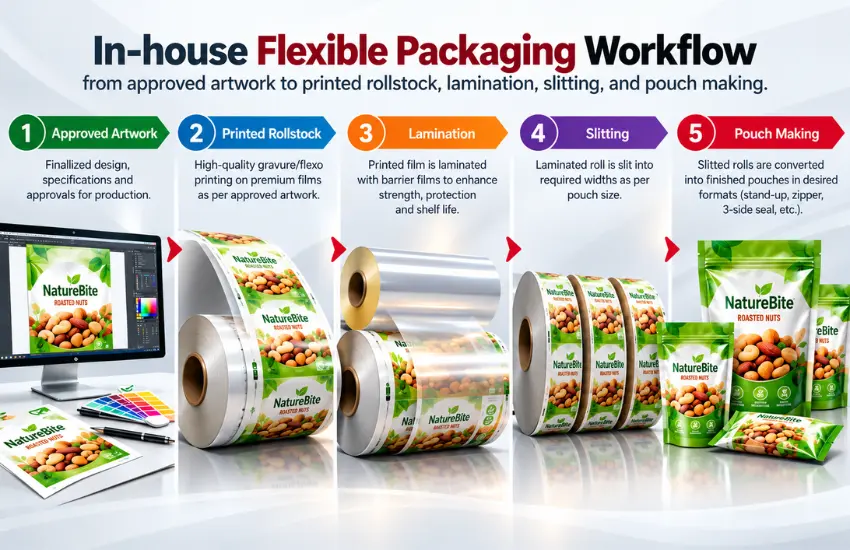
Approved artwork moves from your version-controlled prepress into a print job, prints onto qualified flexible substrate as rollstock, then moves into your lamination, slitting, and pouch-making path, internal or with a converting partner.
The buyer profile it suits
High-mix confectionery portfolios with short-to-medium runs, frequent artwork revisions, private-label and club-pack variants of one base product, seasonal SKU waves, and flavor tests that never justified a plate set.
The profile that should not buy it
A small number of long-running core SKUs on one or two stable structures with little artwork churn. That portfolio is better served by a converter relationship, and Arrow would rather say so early than sell against the math.
Specification | Detail |
Print engine | Memjet DuraCore™ technology, CMYK |
Ink | Water-based pigment inks |
Resolution | Up to 1600 x 1600 dpi |
Printing speed | 90, 150, or 195 ft/min options |
Max media width | 800 mm |
Max printing width | 638 mm |
Max roll diameter | 600 mm |
Listed materials | Coated paper, PP, PET, PVC, BOPP, Mylar, Tyvek, and more |
Film substrate preparation | Film substrates require offline pre-treatment |
Power | Three-phase 220V / 400V |
Air source | 6 Bar |
Substrate compatibility and application fit depend on your exact film structures, pouch formats, and finishing plan. Confirm them with Arrow Systems against your candidate films rather than against a general capability description.
Common questions from confectionery packaging, operations, and procurement teams weighing in-house flexible packaging printing.
Printing and pouch making are separable, and most brands do not start with both. A common path is to print rollstock in-house, then send it to a pouch maker for stand-up pouches and gusseted pouches, or feed it directly to a vertical form-fill-seal or flow-wrap line for bars and family bags. That keeps capital and learning curve focused on print and lamination while converting stays with a partner who already holds the tooling. Decide your converting path before installation, because it sets slitting specs, roll sizes, and floor layout.
There is no universal threshold, and any vendor who quotes one is guessing. What matters is the ratio of SKU count and revision frequency to run length per order. Dozens of active SKUs with short reorders, several film structures, seasonal waves, and regular artwork changes build a strong case. A dozen SKUs on long, stable runs and one structure usually does not, regardless of total footage. Run the landed-cost table above against your own converter invoices and overage history before you set a number.
Flexographic and rotogravure presses transfer ink from plates or engraved cylinders, so every artwork revision needs new tooling and setup, and they are most efficient on long runs of a single design. Digital inkjet printing applies the image directly from a file, so an artwork change needs no plates or cylinders, which suits many SKUs, seasonal graphics, and short reorders. Conventional presses generally keep the advantage on long, stable runs. Film structure, surface treatment, lamination, and seal testing still apply to both, so qualify your films either way.
Barrier performance comes from the film structure and lamination, not from the printing method. The real question is whether a given press prints reliably on the structures you have already qualified. That depends on surface treatment, topcoat, ink chemistry, and how the printed web behaves through lamination, forming, and sealing. On the ArrowJet Aqua 800M, film substrates require offline pre-treatment, so surface preparation belongs in your qualification plan. Test on your actual candidate films rather than assuming, and take food-contact, migration, and labeling questions to your film supplier, co-manufacturer, and regulatory counsel before any production commitment.
Keep outsourcing when a handful of core SKUs run long, stable orders on one or two qualified film structures and the artwork changes only once every few years. In that portfolio a converter will beat you on unit cost and you will not recover the capital. Say that out loud before you build the business case.
On the outsourced side, include printed film price, plates or cylinders per revision, minimum-order overage never consumed, obsolescence, freight, warehousing, expedite premiums, and the revenue impact of missed seasonal windows. On the in-house side, include equipment and training, consumables, prepress labor, floor space, maintenance, and qualification scrap. If the totals land within a few percent of each other, the honest answer is not yet.
The go/no-go decision rests on five reads: SKU churn, run length, film structures, obsolescence, and process discipline.
Score in-house on most of those and the capital case is real. Score a few long-running core SKUs on stable film and your converter is still the right answer.
Bring your SKU list, run lengths per order, recent converter invoices, minimum-order terms, and current film structures, and Arrow Systems will work through a readiness and landed-cost review with you. If the answer is that you are not ready, Arrow will say so and name what to fix first.
Choose the starting point that fits:
Include your name, company, email, phone, SKU count, and current annual printed film spend when you get in touch.
Table of Contents Is Your Confectionery Brand Ready to Bring Flexible Packaging In-House? In-house flexible packaging pays off for confectionery brands with many SKUs, short
Table of Contents Label Slitting and Matrix Removal: Where Converters Lose Finishing Time Label slitting and matrix removal, plus rewinding, cost converters more finishing time
Table of Contents Limited Edition Spirits Label Printing: 4 Holiday Delay Fixes Limited edition spirits label printing runs late because of the calendar, not the
Table of Contents Section 179 Label Printer Timing: Install Before December 31 A section 179 label printer purchase counts for 2026 only if the press
Table of Contents Beer Label Curling in Cold Storage: Diagnose the Mismatch Beer label curling in cold storage signals a facestock, adhesive, or application mismatch
Table of Contents Paper vs. Film Labels: A Substrate Buyer’s Guide Paper wins on cost and aesthetics in dry, indoor conditions; film wins wherever moisture,