Water-Based vs UV-Cured Label Adhesive: Food & Pharma Guide
Table of Contents Water-Based vs UV-Cured Label Adhesive: Food & Pharma Guide Water-based adhesives suit dry, ambient containers; UV-cured hot melts suit cold, wet, curved
Water-based adhesives suit dry, ambient containers; UV-cured hot melts suit cold, wet, curved plastics. Neither is inherently food safe.
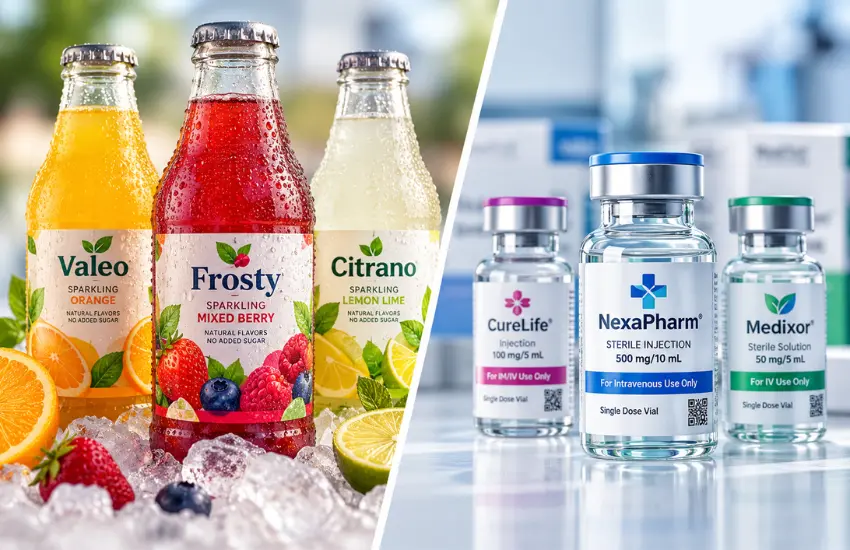
Adhesive failures in food, beverage, and pharma labeling come from cold, condensation, and curvature, not from the printing step.
This guide is written for packaging engineers, quality, and regulatory teams in food, beverage, nutraceutical, and pharmaceutical operations that specify self adhesive labels, also called pressure sensitive labels. The failure patterns are familiar. A juice bottle labeled at 38°F in a condensation-heavy zone lifts a quarter inch in the retail cooler. Bottle label adhesive is judged there, not on the line. A 2 mL vial at -20°C curls at the corners and pulls the barcode out of scanner range.
Neither failure is a printing problem, and both are what push teams to compare water based vs UV cured label adhesive in the first place. You will leave with how each chemistry is built, where migration risk originates, the documentation to demand from suppliers, and a five-step workflow for choosing the right adhesive for labels and locking a defensible label stock specification.
Water-based adhesives dry from an acrylic emulsion; UV-curable hot melts are 100% solids that crosslink under UV energy after hot application.
Both chemistries serve as the adhesive layer in pressure sensitive adhesive labels, so the choice is made at the construction level, together with the facestock and liner.
Water-based adhesive structure
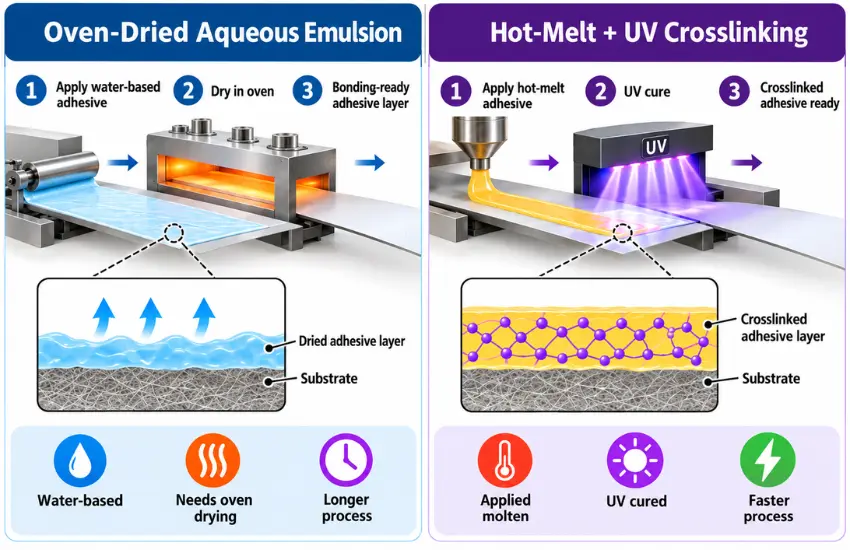
Water-based pressure sensitive adhesives, also called aqueous or emulsion adhesives, start as acrylic polymer particles dispersed in water. The dispersion is coated onto a liner or facestock, then driven through a drying oven. The water evaporates and the polymer particles coalesce into a continuous tacky film.
What stays in the dried film
The dried film contains the acrylic polymer plus whatever was formulated in: surfactants that stabilize the emulsion, tackifying resins that boost initial grab, and sometimes crosslinkers that raise shear strength. Surfactants come up most often in migration discussions because they are relatively low in molecular weight and mobile.
In-service behavior
Aqueous acrylics behave predictably. Clarity is typically good, UV and aging resistance are strong, and adhesion builds over hours rather than instantly. The tradeoff is moisture sensitivity, both during coating and in service. On a wet or condensation-covered container, water at the bond line interferes with wet-out and the label never develops full adhesion.
Typical food and nutraceutical uses
Aqueous chemistry is the default for a large share of adhesive food labels and nutraceutical labeling: dry goods cartons, supplement bottles stored at room temperature, ambient glass and PET, and paper facestock work where cost per square inch and documentation familiarity both favor an established construction.
UV-curable hot melt structure
UV-curable hot melt adhesives are 100% solids systems, with no water and no solvent carrier. They are applied hot as a molten film and then exposed to UV energy. Photoinitiators absorb that energy and trigger crosslinking of the polymer backbone, converting a soft hot melt into a network structure.
Performance advantage of crosslinking
The crosslinked network delivers higher shear strength, better resistance to cold flow and oozing, and a wider usable temperature range at both ends. That is why UV-curable constructions are typically specified for high temperature adhesive labels on hot-fill and pasteurized products. UV-curable systems also tend to grab aggressively on low-surface-energy plastics such as HDPE and polypropylene, and they resist the peel forces generated when a label wraps a small-diameter vial or ampoule.
Cure completeness as the controlling variable
Under-cured adhesive retains unreacted oligomers and residual photoinitiator — exactly the low-molecular-weight species that migration and extractables reviews focus on. Photoinitiator selection, lamp output, and line speed during coating therefore carry compliance implications, not just performance ones. Cure control is a converting process question, and it belongs in supplier qualification.
Where UV-curable chemistry earns its premium
UV-curable chemistry earns its premium in beverage cold chain, chilled and frozen foods, squeezable HDPE containers, and pharmaceutical primary containers where labels must survive autoclave cycles, cryogenic storage, or repeated isopropyl wipe-down. Freezer adhesive labels in particular have to hold through condensation and deep cold, which is where aqueous grades not formulated for cold application tend to flag.
The two chemistries differ on tack, temperature range, wet-surface tolerance, plastics adhesion, wipe-down resistance, and converting behavior.
Attribute | Water-Based (Aqueous Acrylic) | UV-Curable Hot Melt |
Initial tack | Moderate; builds over hours | High; aggressive immediate grab |
Ultimate adhesion | Strong on clean, dry, high-energy surfaces | Strong across a wider surface range |
High temperature resistance | Moderate; can soften under sustained heat | Better; crosslinking resists shear at temperature |
Low temperature / freezer | Formulation-dependent; cold-apply grades needed | Generally broader cold performance |
Wet or condensation-covered surfaces | Sensitive; wet-out is often compromised | Typically more tolerant |
Low-surface-energy plastics (HDPE, PP) | Weaker unless specifically formulated | Usually stronger |
Solvent and wipe-down resistance | Moderate | Better; crosslinked film resists IPA attack |
Clarity for clear-on-clear | Typically excellent | Good; varies by grade |
Die-cutting and matrix strip | Clean; well understood in converting | Can require tuning; ooze risk if under-cured |
Repositionability | Some grades are sold as removable adhesive labels or repositionable options | Mostly sold as permanent adhesive labels |
Treat this table as a starting point for your own trials, not a specification. The comparison is qualitative and directional only.
Failure modes worth naming in a trial protocol: flagging and edge lift on curved containers, adhesive ooze onto die stations and applicator parts, ghosting or residue on returnable glass, adhesive transfer during removal, and cold flow that lets a label creep on a small-radius surface.
Migration is a property of the whole label construction, not the adhesive alone; both chemistries can be compliant or non-compliant.
Direct answer: Migration is a system property, not an adhesive property. Risk depends on the adhesive layer, the barrier performance of the facestock, whether contact is direct or indirect, and the application and service conditions. Both aqueous and UV-curable constructions can be compliant or non-compliant depending on build and use.
Most pressure sensitive labels on food packaging are an indirect food contact application. The adhesive sits on the outside of a container wall or carton, and the container itself is the barrier. The working question is whether the facestock, ink, and container together block migration of adhesive components into the food.
The functional barrier concept is central. A metallized or polymer film facestock on a glass bottle presents a very different migration pathway than porous uncoated paper applied to a thin-wall squeezable pouch. Set-off during roll storage and diffusion through low-barrier substrates are both plausible routes, and neither depends on which chemistry you picked.
Fatty and oily products
Fats are aggressive extractants for many adhesive components, so fatty and oily products raise migration risk.
Hot-fill and pasteurization
Elevated temperature during hot-fill and pasteurization accelerates diffusion of adhesive components.
Acidic products
Acidic products such as juice, sauces, and kombucha belong in the migration risk map.
Thin-wall and flexible packaging
Squeezable bottles, pouches, and films have limited barrier, so the container offers less protection against migration.
Porous or uncoated substrates
Paperboard sleeves and kraft wraps are porous, which gives adhesive components an easier path through the substrate.
Long shelf life
Migration accumulates over time, so a longer shelf life increases exposure.
U.S. frameworks
The U.S. indirect food additive provisions for adhesives in 21 CFR Part 175 and FDA’s food contact substance notification program describe how adhesive components used in food packaging are evaluated.
EU frameworks for exported SKUs
Exported SKUs may also be assessed against EU Regulation 1935/2004 and, where plastics are involved, Regulation 10/2011.
Why no adhesive is “FDA approved” on its own
These frameworks evaluate substances within a defined use, which is why no adhesive can be meaningfully described as “FDA approved” as a standalone material.
How to read supplier compliance statements
A supplier statement typically confirms that a formulation’s components are addressed under named regulations for a described use condition. It is not a blanket clearance, and it does not transfer responsibility for the finished package. That determination stays with the brand owner or manufacturer, informed by supplier documentation.
In GMP operations, label adhesive sits inside a controlled specification, so any change goes through GMP change control, not purchasing.
Why adhesive is a controlled component
In a GMP environment, the technical comparison is only half the work. Pressure sensitive label stock is a specified component, and expectations under 21 CFR Parts 210 and 211 mean the adhesive generally sits inside a controlled specification. It is not an interchangeable commodity a converter can substitute mid-year, which makes an adhesive swap a GMP change control event rather than a purchasing decision.
What an adhesive change can trigger
Under a documented GMP change control process, an adhesive change may trigger specification revision, supplier qualification activity, retention sample updates, stability or transport assessment, and potentially requalification of the labeling operation. Change control in GMP settings expects the change, its risk assessment, and its approval to be documented before the new stock is used. Teams that treat an adhesive swap as a purchasing decision usually discover the documentation cost afterward.
Extractables and leachables on primary containers
When the label sits on a primary container — a vial, ampoule, prefilled syringe, or blister card — extractables and leachables thinking extends to the label construction. The questions are whether adhesive components can migrate through the container wall or closure system, and whether the facestock and ink contribute to the extractables profile. Extractables are what a material can release under aggressive laboratory conditions; leachables are what actually migrates into the product in normal storage and use.
Lifecycle conditions adhesion must survive
Adhesion has to hold across terminal sterilization or autoclave cycles, 2–8°C cold chain with repeated condensation events, -80°C or liquid nitrogen storage, small-diameter curved surfaces, and isopropyl or quaternary disinfectant wipe-down in clinical settings.
Serialization and scanning requirements
Serialization and unit-dose formats add a scanning requirement, so legibility and flatness matter as much as bond strength.
Specify label adhesive in five steps: worst case, condition matrix, documentation, bench and line trials, then a locked construction.
Step 1: Define the worst-case contact and service scenario
Use the worst case, not the typical case: the hottest fill, the coldest storage, the wettest bottle, the most aggressive product. Work one SKU family at a time.
Step 2: Build a condition matrix
For each SKU group, document container material and surface energy, container surface temperature at application, moisture or condensation at application, service temperature range and duration, chemical exposure (product contact, disinfectants, ice slurry), required shelf life, contact classification, and end-of-life recyclability requirements. This matrix is what a converter or adhesive supplier needs before recommending a construction.
Step 3: Request documentation before sampling
Use the supplier documentation checklist above. If a supplier cannot produce a regulatory compliance statement or a change-notification commitment, that is a finding, not a delay.
Step 4: Run bench and line trials
At minimum: 24-hour and 7-day peel on the actual container, cold-room hold at your storage temperature, condensation soak with labels applied to chilled containers, isopropyl wipe-down and abrasion checks, and a full-speed line trial through your applicator with observation of matrix strip and any adhesive ooze. Hold samples for the product shelf life where feasible.
Step 5: Lock the specification under change control
Record facestock, adhesive, liner, and print method together as one construction. Adhesive performance depends on the whole laminate, so approving components separately invites a silent substitution later.
Why digital production pushes constructions to converge
Adhesive and liner choices interact directly with your automation roadmap. On-demand digital label printing turns pressure sensitive label printing into a short-run, per-SKU process, so you can retire obsolete pre-printed inventory. For digital pressure sensitive labels for pharma and food alike, it also pushes your constructions to converge. High-changeover schedules reward a small set of validated constructions that cover clustered condition profiles rather than a unique stock per SKU.
The ink layer is part of the construction
The printed ink sits in the same stack as the adhesive, facestock, and liner, so it affects the migration picture too. The ArrowJet Aqua 330R prints with water-based pigment inks on a Memjet DuraFlex® engine and is Nestlé Guidance compliant, so food and beverage teams that print their own labels start from an ink set that meets that guidance. The finished construction still needs its own migration assessment, so test printed samples on your actual container and product.
Include finishing in the line trial
Matrix strip behavior and adhesive ooze onto die stations only show up on the finishing equipment you actually run, so include die-cutting and slitting in the line trial. For short-run, high-changeover production, pairing your digital press with Arrow’s label finishing systems lets you run that trial across the full print-and-finish path.
Match adhesive to service conditions: water-based for ambient dry goods, UV-curable for cold, wet, curved, or demanding pharma containers.
Aqueous acrylic typically fits
Ambient-temperature glass and PET, dry goods and paperboard, supplement and nutraceutical bottles, clear-on-clear film labels where optical quality drives the spec, applications needing removability or clean release, and programs where an established, well-documented water based pressure sensitive adhesive construction lowers qualification effort.
UV-curable hot melt typically fits
A UV curable hot melt adhesive suits chilled and frozen beverage and food, HDPE and polypropylene containers, small-diameter vials and ampoules, labels exposed to disinfectant wipe-down, hot-fill and pasteurized products, and pharmaceutical primary containers with demanding thermal cycles.
Evaluate a different construction entirely when
One SKU must span both ambient application and deep-freeze service (consider a validated all-temperature adhesive), the container geometry defeats any flat label (consider shrink sleeve or in-mold labeling), the container is returnable or reusable with residue constraints, or recyclability targets call for a wash-off adhesive system.
Common questions from packaging, quality, and regulatory teams comparing label adhesive chemistries for food and pharmaceutical use.
No. Neither chemistry is inherently safer. Migration potential depends on the specific formulation, the barrier performance of the facestock and container, whether the application is direct or indirect food contact, and the product and service conditions. A well-documented aqueous acrylic under a film facestock on glass and a fully cured UV-curable adhesive can both be appropriate. An under-cured UV film or a heavily surfactant-loaded emulsion under porous paper on a fatty product can both raise legitimate concerns. Evaluate the construction in its intended use, supported by supplier documentation.
Usually some level of assessment, yes. Because label stock is generally a controlled component, an adhesive change is evaluated through your GMP change control procedure rather than handled as a purchasing substitution. Depending on risk, that can include specification revision, supplier qualification, updated compliance documentation, adhesion and legibility testing across storage and distribution conditions, extractables assessment for primary container labels, and retention sample updates. Scope the change-control impact before you approve samples. It often shifts the economics of a chemistry switch more than unit price does.
UV-curable hot melt constructions usually hold an advantage. Aqueous emulsions depend on wet-out at the bond line, and condensation plus a surface below the adhesive’s minimum application temperature both suppress bond formation. That combination is the common cause of flagging on chilled beverage bottles. Aqueous adhesives formulated specifically for cold and moist application do exist and perform well within their stated limits. Verify with a condensation soak trial and a cold-room hold on your actual container at line temperature rather than relying on the data sheet range.
Request six items: a technical data sheet with the service temperature range and minimum application temperature; a regulatory compliance statement naming the frameworks and use conditions evaluated; a statement of composition or component disclosure where the supplier will provide it; lot traceability from adhesive coater through converting; a written change-notification commitment covering formulation, coater, and raw material source changes; and cure process control information for UV-curable constructions. If a supplier cannot produce a compliance statement or a change-notification commitment, treat that as a finding, not a delay.
Extractables are compounds that can be pulled out of a label material under aggressive laboratory conditions, such as strong solvents or heat. Leachables are the compounds that actually migrate into the product under normal storage and use. Extractables and leachables testing therefore usually starts with a worst-case extractables study and then confirms what appears in the product over its shelf life. For labels on primary containers, the scope is set by the drug product owner’s quality and regulatory team, supported by supplier documentation.
Food contact, extractables, and GMP compliance determinations are the responsibility of the brand owner or manufacturer and should be confirmed with qualified regulatory and quality professionals. Arrow Systems sells digital label printing and finishing hardware; Arrow does not provide regulatory or compliance advisory services.
If your food, beverage, nutraceutical, or pharmaceutical operation is moving label production in-house or consolidating label constructions across SKUs, Arrow Systems offers a structured, no-obligation assessment for packaging, operations, and quality leaders.
The assessment reviews your SKU count, run lengths, label formats, and finishing needs to recommend a digital press and finishing configuration that fits your validated label constructions and changeover schedule.
Table of Contents Water-Based vs UV-Cured Label Adhesive: Food & Pharma Guide Water-based adhesives suit dry, ambient containers; UV-cured hot melts suit cold, wet, curved
Table of Contents Is Your Confectionery Brand Ready to Bring Flexible Packaging In-House? In-house flexible packaging pays off for confectionery brands with many SKUs, short
Table of Contents Label Slitting and Matrix Removal: Where Converters Lose Finishing Time Label slitting and matrix removal, plus rewinding, cost converters more finishing time
Table of Contents Limited Edition Spirits Label Printing: 4 Holiday Delay Fixes Limited edition spirits label printing runs late because of the calendar, not the
Table of Contents Section 179 Label Printer Timing: Install Before December 31 A section 179 label printer purchase counts for 2026 only if the press
Table of Contents Beer Label Curling in Cold Storage: Diagnose the Mismatch Beer label curling in cold storage signals a facestock, adhesive, or application mismatch